SMT Quality Inspection Standards
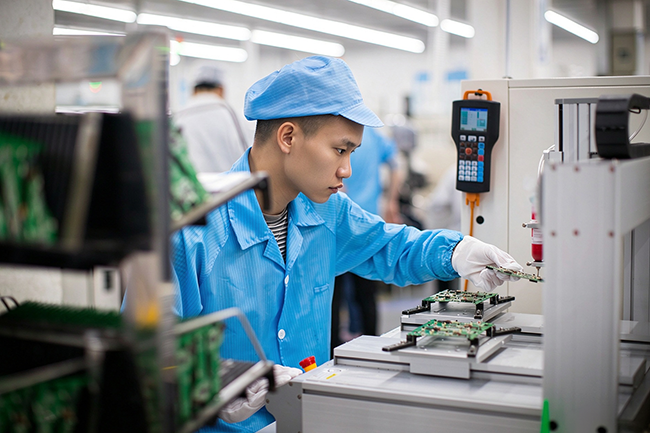
'We inspect everything' is the easiest claim to make and the easiest to fake. Real SMT quality is defined by which defects you look for, with what tools, and against which standard. At KOMKIA it is IPC, every line, every shift.
The inspection ladder
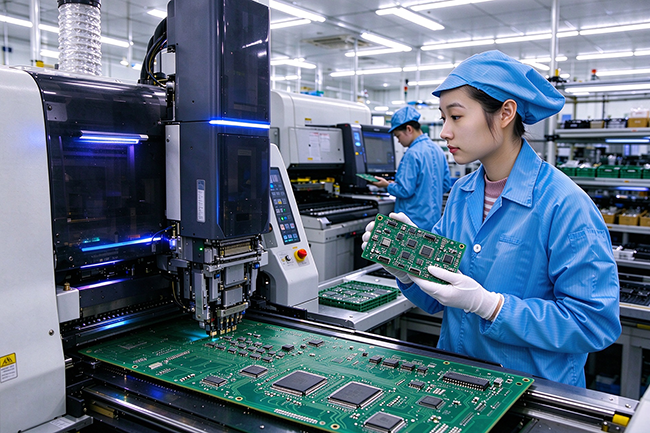
A robust line layers inspection rather than relying on one gate. Solder paste inspection (SPI) catches volume and alignment before placement. Automated optical inspection (AOI) catches bridging, missing and misaligned parts after reflow. And selective X-ray verifies hidden joints under BGAs and QFNs.
- SPI — paste volume, height and offset
- AOI — bridges, tombstones, missing/skewed parts, polarity
- X-ray — BGA/QFN voids and hidden solder joints
- ICT / functional test — electrical correctness
What 'acceptance' actually means
Per IPC-A-610, a joint is acceptable when wetting is evident, fillet size is within limits, and there are no forbidden defects (cracks, dewetting, foreign material). 'Looks shiny' is not a criterion. Our operators are trained and re-certified against the same class your product requires — typically Class 2, Class 3 for mission-critical.
Avoiding the false-pass trap
AOI thresholds set too loose miss defects; set too tight they bury inspectors in false alarms. We tune per product family and review escape data weekly. The metric that matters is escaped defects at functional test, not AOI pass rate.
Key takeaways
Key Takeaways
- Layer SPI, AOI and X-ray instead of trusting a single gate.
- Acceptance is judged against IPC-A-610 class, not 'shininess'.
- Tune AOI to minimize escaped defects, not to maximize pass rate.